
Wilmington Foods FZE – Sharjah, United Arab Emirates
Tahini & Halwa Production Lines – Complete Industrial Automation Solution
The Challenge:
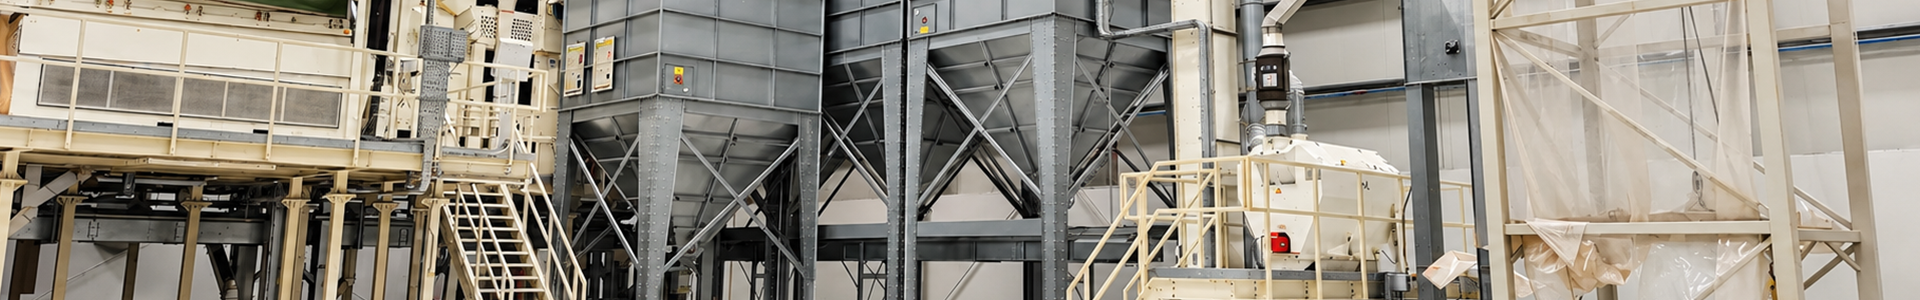
Wilmington Foods FZE undertook a phased modernisation of its tahini and halva production facilities in Sharjah to improve production efficiency, process consistency, and operational reliability. The aim was to move from manual, operator-driven production to a centrally controlled, digitally monitored plant built on a single standardised automation platform. The main challenge was to automate two independent production lines while integrating third-party OEM machine PLCs from different manufacturers. The halva line expansion also had to be implemented without disrupting the already operating tahini line. The project required a reliable industrial communications backbone for a large number of intelligent field devices, centralised monitoring and control, and an architecture that could support future production expansion.
The Solution:
Velox Automation delivered a complete Siemens-based automation solution for both production lines, including engineering, PLC and SCADA software development, industrial network design, commissioning and support. This area includes Siemens ET200SP PLCs, TIA Portal Engineering with migration from V17 to V20, WinCC Professional SCADA upgraded from V17 to V20, KTP1200 and MTP1500 Unified HMIs, 17 ABB VFDs, and 17 Siemens SIMOCODE pro C iMCC on PROFINET and PROFIBUS networks. Third-party machine PLCs from Bühler, Maseto, and Nasbad were also integrated into this solution. Automated process sequences were developed for ingredient transfer, cooker operation, recipe handling, buffer tank management, product filling, cooling, and utility control. The halva line expansion was implemented while keeping the existing tahini line operational, minimising disruption to ongoing production.
Why Velox Solutions Makes Sense
For the Client:
The projects enabled Wilmington Foods to transform its tahini and halva facilities into a modern, digitally controlled production environment based on a certified automation platform.
Key benefits included:
- Standardised PLC, HMI and SCADA architecture across both production lines
- Improved production consistency, repeatability and process control
- Centralised plant monitoring and enhanced process visibility
- Improved equipment diagnostics and faster troubleshooting through intelligent drives and motor management
- Reliable industrial communication and integration of third-party machine PLCs
- Reduced manual intervention and simplified maintenance
- Improved operator productivity through automated process sequencing
The new automation platform provides Wilmington Foods with a reliable and scalable foundation for efficient plant operation and future capacity growth.
For the Environment:
At Velox Automation, sustainability is considered part of every one of our projects. By replacing manual operations with automated sequencing and accurate recipe control, the solution helps reduce process deviations, product rejections, rework, and raw material waste. Variable frequency drives and intelligent motor management enable optimised equipment operation and support efficient energy use in production lines. Together, these measures contribute to efficient plant operations while supporting Wilmington Foods’ sustainability objectives.